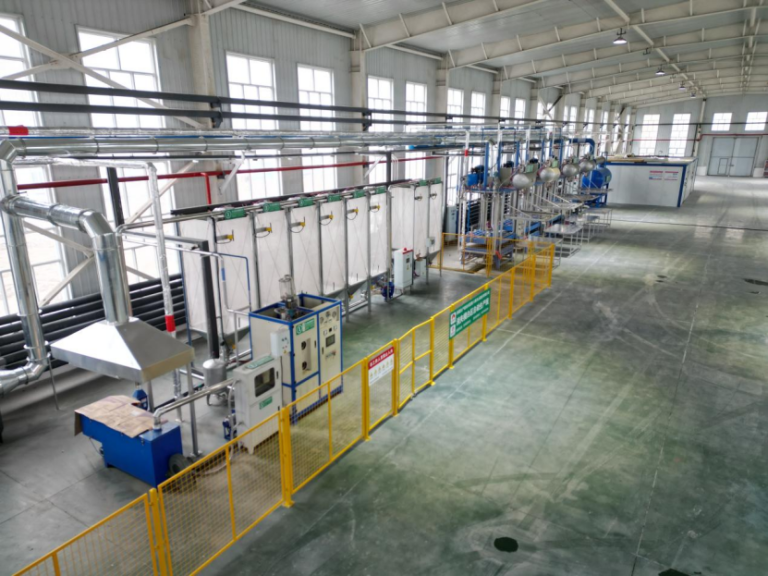
Automated Lost Foam Casting (LFC) Production Line
Turnkey automated line featuring cluster drying, 3D multi-frequency sand compaction table, automatic flask negative pressure docking, and centralized sand regeneration.
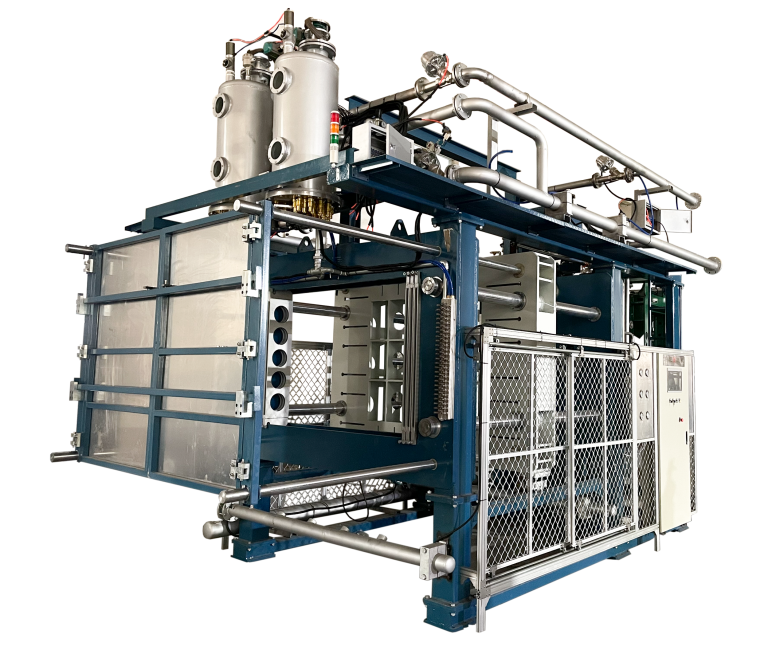
Horizontal EPS Pattern Molding Machine
Precision hydraulic horizontal molding unit for complex engine blocks and cylinder head patterns. Equipped with Japanese steam balance valves and fast mold cooling.
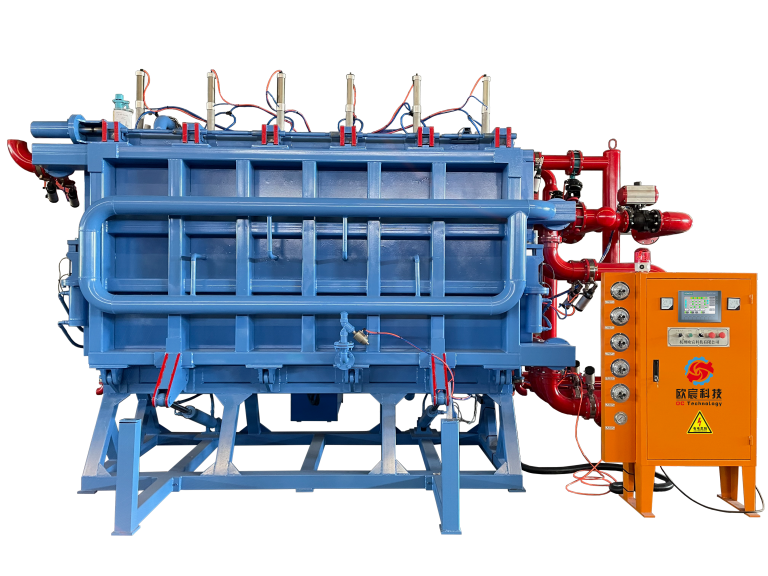
Copolymer Large Foam Block Molding Machine
Engineered for STMMA / EPS / PMMA copolymer pattern blocks used in large structural castings. High vacuum condensing system ensures moisture content under 1.5%.
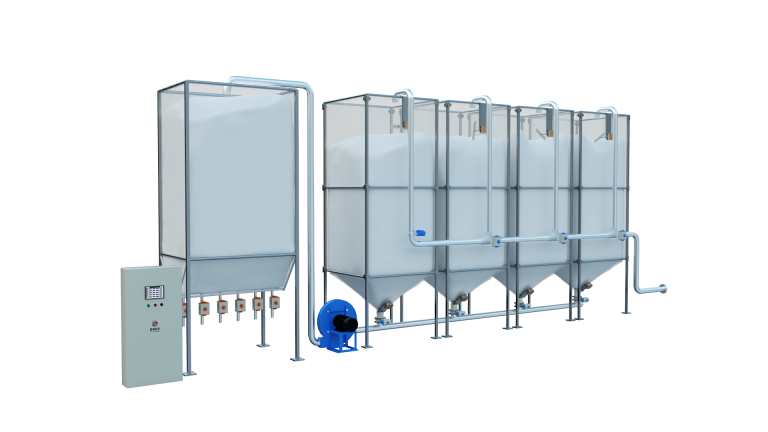
Automated Bead Maturation Silo System
Centralized storage and aging silo cluster. Incorporates anti-static breathable liners, automated air blowing, and proportional pipe switching to molding stations.
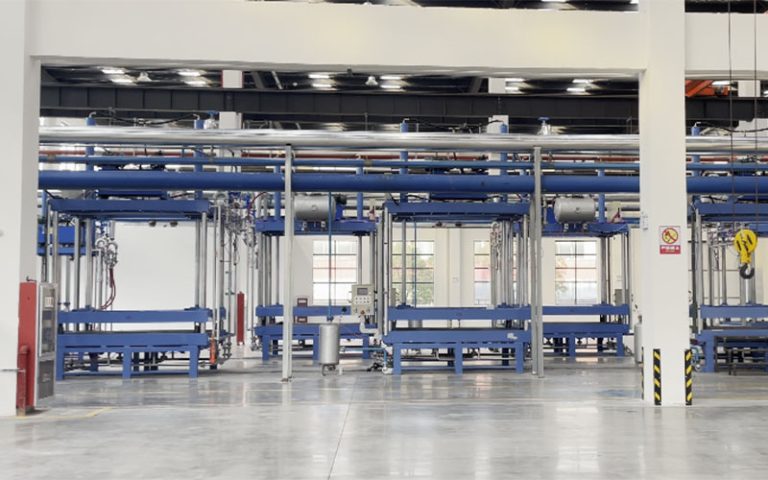
V-Process Automated Turnkey Production Line
Binder-free vacuum sealing casting line. Films thermoform tightly against the pattern while dry sand is compacted by vacuum negative pressure. Exceptional surface finish.
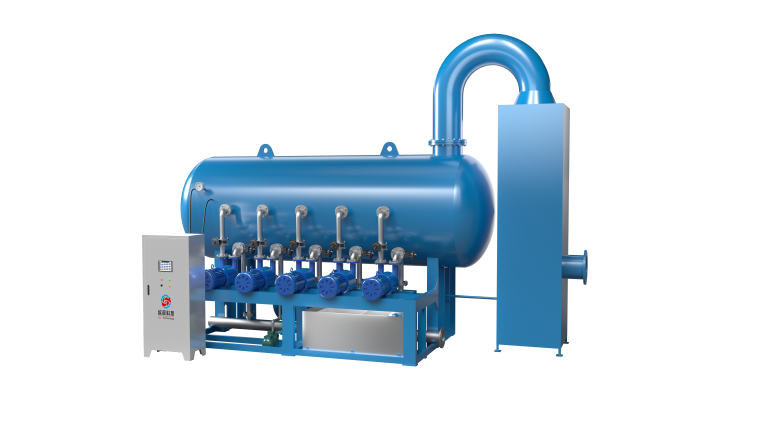
Central Vacuum Negative Pressure Station
Multi-pump liquid ring vacuum array with dual surge buffer tanks and electronic proportional regulation. Maintains stable mold negative pressure during high-temp pouring.
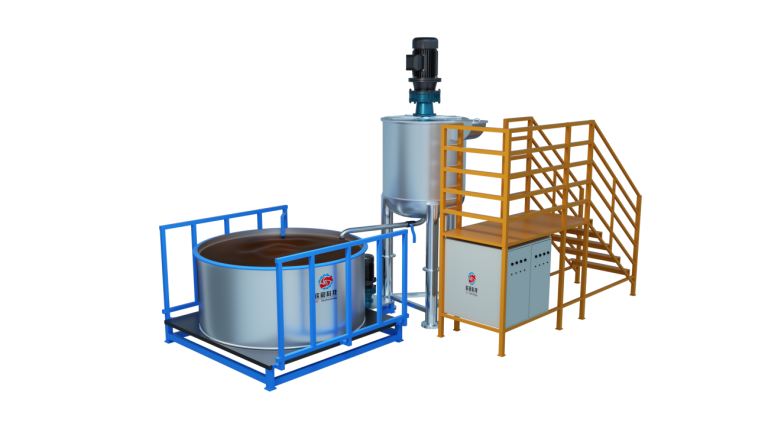
Continuous Bottom-Discharge Pre-Foamer
Precision batch pre-expander featuring electronic weighing, steam proportional ramp-up, and fluidized bed drying to produce perfect uniform beads without clumping.
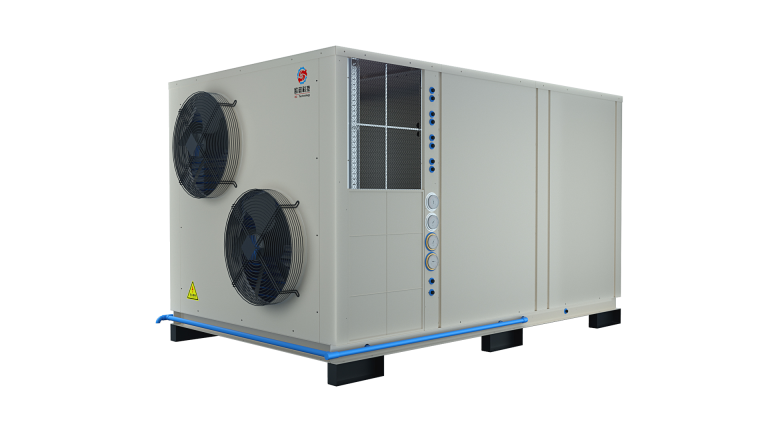
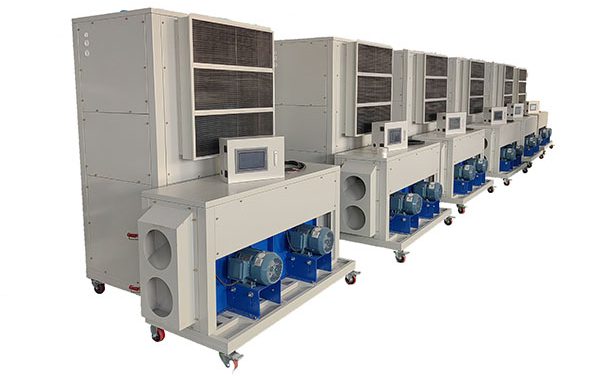
Top-Mounted Heat-Pump Pattern Dryer
Dehumidifies and cures refractory ceramic paint on foam clusters without thermal deformation. High-velocity laminar airflow cuts cluster drying time to 2-3 hours.
Lift-Type Refractory Paint Mixer
Dual-speed high-shear dispersion mixer for preparing lost foam alcohol-based and water-based zircon coatings. Prevents settling and bubbles in dipping tanks.
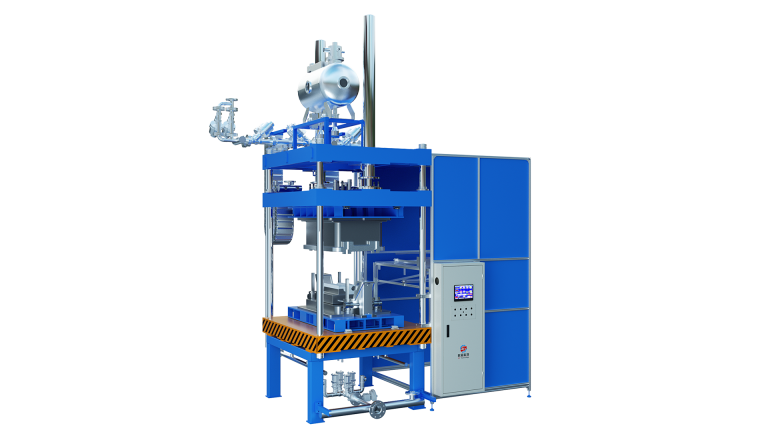
Vertical Precision Foam Molding Machine
Vertical clamping machine with ergonomic low-level pattern ejection. Ideal for valve bodies, pipe fittings, and small engine components with quick mold changeover.